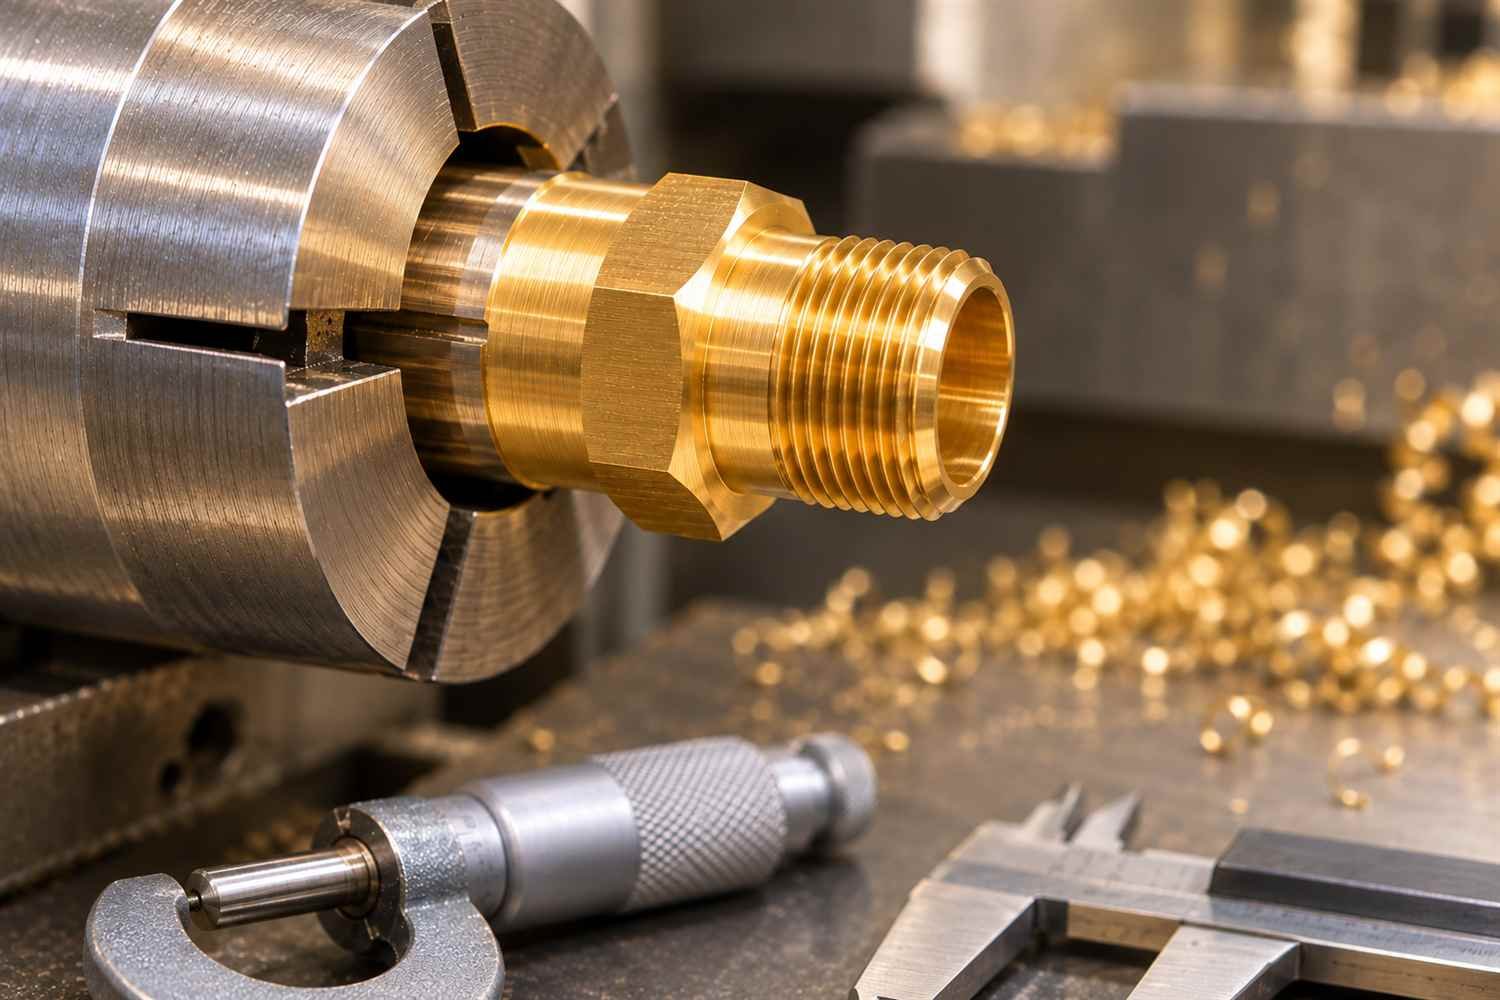
Precision turned brass tolerances and surface finish decide whether a fitting seals, a shaft turns freely, or an assembly jams on the line. This guide explains how buyers can specify fit, seal and finish on turned brass components without paying for precision nobody asked for.
Quick answer: Use ISO 2768-m as the general tolerance block, then call out ISO 286 fits such as H7 or h6 only on features that mate, seal or locate. Specify Ra in micrometres only where finish affects function; keep as-turned brass at Ra 0.8 to 1.6 µm. Tightening everything to ±0.005 mm or Ra 0.2 µm multiplies cost with no functional gain.
What general tolerance should a precision turned brass drawing use?
ISO 2768 is the familiar international system for general, individually untoleranced linear and angular dimensions on machined parts. The traditional grades are v (very coarse), c (coarse), m (medium) and f (fine). For precision turned brass components, ISO 2768-m is the sensible default for most commercial work, and ISO 2768-f is reasonable when the part feeds a sealing or locating assembly. The current edition is ISO 2768:2026, so new drawings should state the edition as well as the grade.
A general tolerance block replaces dozens of repetitive callouts. It covers the dimensions you did not tolerance individually, which keeps the bulk of the part economical and leaves room to tighten the few features that actually matter. For LPG parts, this produces a clearer quotation.
What is the difference between ISO 2768 and ISO 286?
ISO 2768 governs general dimensions. ISO 286 defines the limit-and-fit system for mating features, such as an H7 bore accepting a g6 shaft. The current reference is ISO 286-1:2010, confirmed in 2026. Use ISO 2768-m for the part as a whole, then mark specific diameters with ISO 286 fit symbols where a clearance, transition or interference fit is required.
This distinction is the single most useful habit in specifying turned brass: general tolerance on the frame, fit tolerance on the feature.
Which tolerances are realistically achievable on precision turned brass?
Achievable tolerance depends on the machine, alloy, feature geometry and inspection method, not on wishful thinking. The figures below are typical production capability for free-machining brass such as CW614N (CuZn39Pb3) or CW617N (CuZn40Pb2), with workpiece diameters in the 2 to 32 mm range and first-article inspection in place.
| Machine route | Turned diameter | Bored ID | Surface finish Ra |
|---|---|---|---|
| Multi-spindle screw machine | ±0.05 to ±0.10 mm | ±0.10 mm | 0.8 to 1.6 µm |
| Single-spindle CNC turning | ±0.02 to ±0.05 mm | ±0.02 mm | 0.4 to 1.6 µm |
| Swiss-type sliding-headstock CNC | ±0.005 to ±0.02 mm | ±0.008 mm | 0.2 to 0.8 µm |
| Swiss CNC plus grinding finish | ±0.002 mm | ±0.002 mm | 0.05 to 0.2 µm |
Thin walls, long slender features, interrupted cuts and plating allowances all reduce capability.
How do precision turned brass tolerances affect the cost of a part?
Over-specification is the main avoidable cost driver in precision brass. The relative cost index below uses ISO 2768-c on a multi-spindle screw machine as 1.0; it is a planning guide, not a quotation.
| Tolerance specification | Relative cost index |
|---|---|
| ISO 2768-v (very coarse) | 0.9 |
| ISO 2768-c (coarse) | 1.0 |
| ISO 2768-m (medium) | 1.1 |
| ISO 2768-f (fine) | 1.4 |
| Selected features at IT7 / H7 | 1.2 to 1.5 |
| Selected features at IT6 / h6 | 1.6 to 2.0 |
| Selected features at IT5 (±0.005 mm) | 2.2 to 3.0 |
| Whole part at IT5 | 3.5 to 5.0 |
| Grinding finish on a critical diameter | +0.5 to 1.0 on top of base |
The pattern is clear: tightening the whole part is expensive, tightening one feature is usually affordable. The right question on every drawing is not “how tight can we go?” but “which feature actually needs to be tight?” That habit helps RFQ reviews for automotive brass components.
What surface finish should you specify on turned brass?
Surface finish is commonly measured as Ra, the arithmetic average roughness in micrometres. As-turned free-machining brass naturally finishes at Ra 0.8 to 1.6 µm, which is adequate for most functional surfaces. Specify Ra 0.4 µm only where a seal, bearing surface or sliding fit depends on it, and Ra 0.2 µm only for cosmetic or special contact surfaces.
Define Ra only where it affects fit, sealing, wear or appearance, and state whether tolerances apply before or after plating. For pneumatic parts and gas fittings, the sealing face and thread flank usually earn the tighter finish.
How should a buyer write a clean tolerance block and avoid over-paying?
A well-written tolerance block answers four questions in a few lines: the general standard, the surface finish default, edge condition and thread standard. A typical block reads:
UNLESS OTHERWISE STATED:
Linear and angular tolerances: ISO 2768-m, edition stated
Geometric tolerances: ISO 2768-K where applicable
Surface finish: Ra 1.6 µm
Edges: deburr, break sharp edges 0.3 mm max
Thread: per ISO 261 / ISO 965, medium fit class 6H/6g
Material: CW614N (CuZn39Pb3) per EN 12164, or CW617N per EN 12164
Plating: none, or specify on the purchase order
Note: all dimensions in millimetres
Critical features that need tighter control are then called out individually, for example a sealing bore marked Ø10 H7 with concentricity 0.01 mm to datum A. Agree the critical dimensions and measurement plan at the RFQ stage, including whether inspection is by calipers, micrometers, pin gauges, thread gauges or CMM.
Premi Brasscom International is a precision-turned metal components manufacturer in Jamnagar since 1984, ISO 9001:2015 and IATF 16949 certified, with 550+ standard products and 300+ custom components. Our quality process and enquiry team can review a drawing against these rules before tooling begins.
Key takeaways
- Use ISO 2768-m as the general tolerance block on the whole drawing; it sets expectations without adding cost to every feature.
- Tighten only mating, sealing and locating features with ISO 286 fits such as H7 and h6; tightening the whole part multiplies cost.
- Keep surface finish at Ra 0.8 to 1.6 µm for as-turned brass and specify Ra 0.4 µm only where function demands it.
- State plating and finishing tolerances as pre-plate or post-plate, and allow for coating thickness on threads.
- Agree critical dimensions and the inspection method at RFQ, then verify with first-article and in-process inspection.
Frequently asked questions
What general tolerance applies to machined brass parts?
ISO 2768 medium “m” or fine “f” is the usual general tolerance for linear and angular dimensions that are not individually toleranced; tighter features are called out specifically with ISO 286 fits.
What is the difference between ISO 2768 and ISO 286?
ISO 2768 covers general untoleranced dimensions. ISO 286 defines the hole and shaft limit-and-fit system, such as H7/g6, for mating features that need a specific clearance or interference.
What tolerances can be held on Swiss-machined brass?
Sliding-head turning routinely holds about ±0.01 to 0.02 mm on small diameters and down to ±0.005 mm on critical slender features; below that, grinding or honing is normally required.
How do I avoid over-paying for tolerances?
Tolerance only the features that matter, use ISO 2768-m as the default block, reserve tight ISO 286 fits for mating surfaces, and agree the measurement plan with the supplier at RFQ.
Sources: ISO 2768:2026 and ISO 286-1:2010, plus practical guides from Brassland, DEK, HPPI, FPE Machining, Ruiyi and Vencomfg.