Dezincification-resistant (DZR) brass is the grade you specify when a brass part will spend its life in contact with potable water. The short answer for buyers comparing the two most common grades: CW602N is dezincification-resistant; CW617N is not. CW602N (CuZn36Pb2As) uses an arsenic inhibitor and a controlled heat treatment to keep zinc loss below the limit set in EN 12164 and EN 12165. CW617N (CuZn40Pb2) is a faster-machining, lower-cost forging brass with no DZR protection at all.
That difference decides whether a fitting survives twenty years or fails behind a wall in five. It also matters for compliance: from 31 December 2026 the European positive lists under the Drinking Water Directive apply to metal components in contact with drinking water, and neither CW602N nor CW617N appears on them. This guide sets out what dezincification actually does, how the two alloys compare, how DZR is proven, and what to write into a purchase order so you get what you paid for.
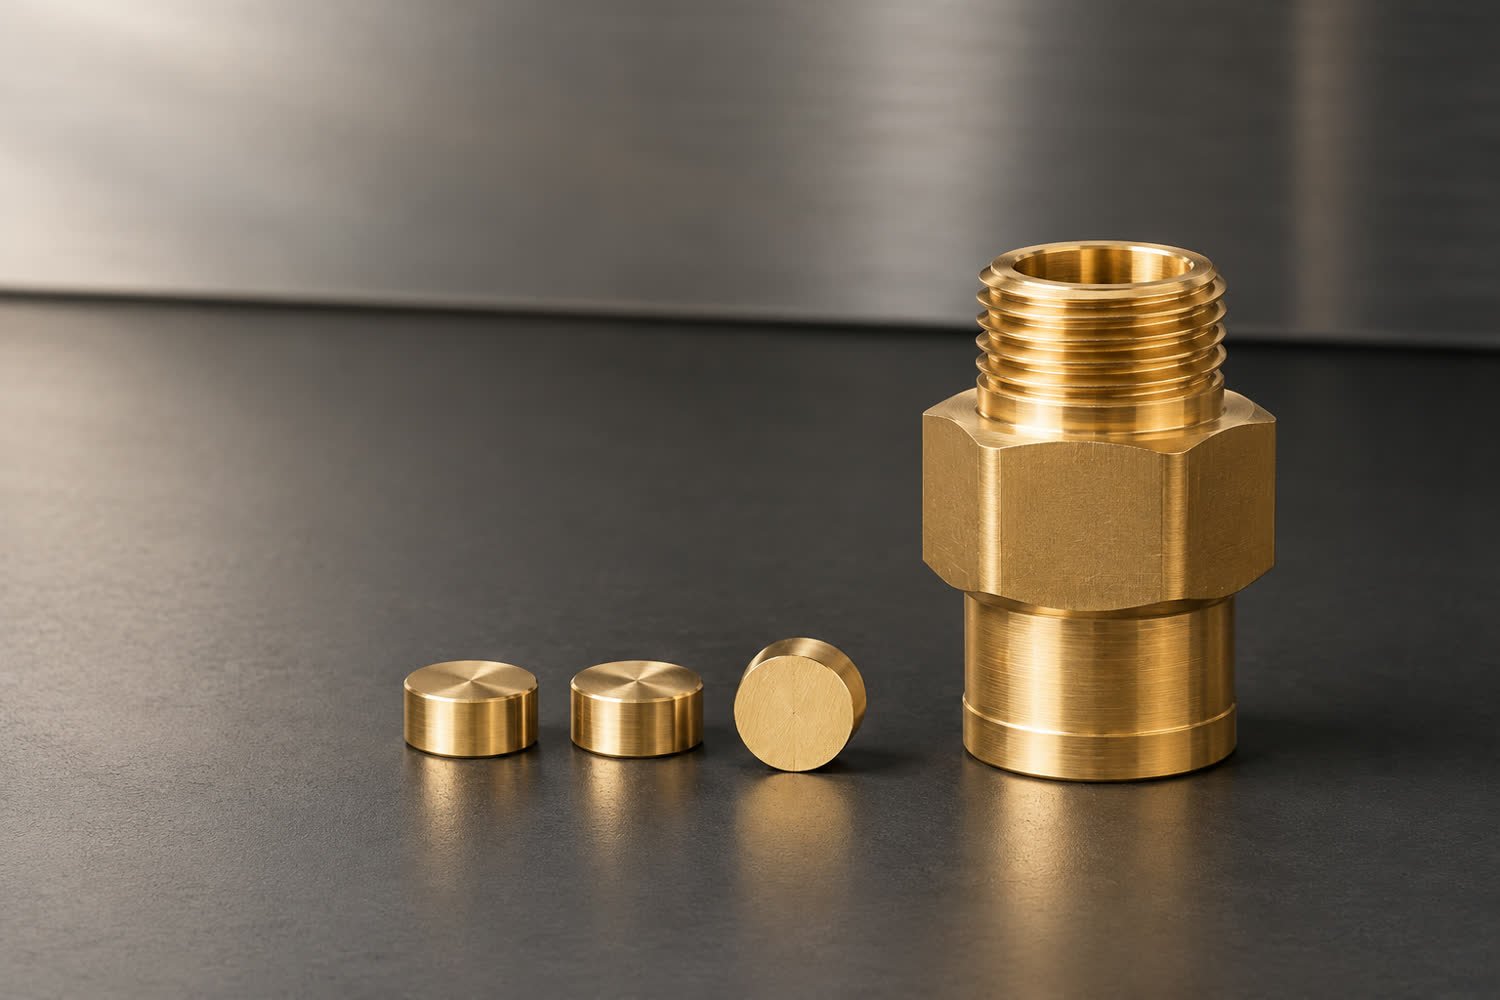
What dezincification does to a brass fitting
Brass is copper plus zinc. In water that is soft, warm, stagnant or high in chlorides relative to carbonate hardness, the zinc can dissolve selectively and leave behind a porous copper sponge that keeps the original shape but has almost no strength. The part looks fine from outside. It fails under pressure, often as a pinhole leak or a split thread.
Two forms matter in procurement:
- Layer dezincification — a uniform band of weakened metal parallel to the surface. Common, and often cosmetic in its early stage, but it thins the pressure-bearing wall.
- Plug dezincification — a localised plug of porous copper that penetrates deep into the section. This is the dangerous one: it produces sudden leaks and thread failures with no visible warning.
Risk rises with pH above about 8, a high chloride-to-carbonate-hardness ratio, temperatures over 60 °C, stagnant or low-flow lines, and soft, low-alkalinity or de-ionised supplies. Any brass with more than about 15% zinc is a candidate; the question is whether the alloy and its processing were designed to resist it.
Which brasses actually resist dezincification
There are two engineering routes, and it helps to know which one your supplier is selling.
Inhibited brass — CW602N (CuZn36Pb2As). A small addition of arsenic (typically 0.02–0.05%) inhibits zinc loss in the alpha phase. Because arsenic only protects alpha, the beta phase must be broken up into isolated islands by a controlled heat treatment, usually 500–550 °C for one to two hours after hot forging, followed by slow cooling in air. This is why DZR is a property of the processed part, not of the bar alone.
Aluminium-bearing DZR — CW625N and CW626N. Forging grades with a wider acceptance limit (200 µm rather than 100 µm). Useful where the part geometry or process suits them, but check the product approval route before switching.
Silicon brass — CW724R (CuZn21Si3P) and the US equivalent C69300. Roughly 21% zinc and no beta phase, so it is dezincification-resistant by composition rather than by inhibitor, and it is lead-free at ≤0.10%. This is the grade that dominates new potable-water designs in the EU and UK, at the cost of harder machining and a higher material price.
CW602N vs CW617N at a glance
| Property | CW602N (DZR) | CW617N (standard) |
|---|---|---|
| Composition | CuZn36Pb2As | CuZn40Pb2 |
| Copper | 61–63% | 57–59% |
| Zinc | Balance (~36%) | Balance (~40%) |
| Lead | 1.7–2.8% | 1.6–2.2% |
| Dezincification resistance | Yes — arsenic inhibited, heat treated | No |
| Max depth, ISO 6509-1 (EN 12164 / 12165) | 100 µm | Not compliant |
| Typical process | Hot forging or machining, then heat treatment | Hot forging and high-speed machining |
| Machinability | Good, slightly below CW617N | Reference free-cutting grade |
| Relative material and process cost | Higher — inhibitor plus heat-treatment step | Lowest |
| Right for | Potable water bodies, concealed fittings, soft-water markets | Neutral hard water, gas, pneumatic, non-wetted parts |
| EU positive list (from 31 Dec 2026) | Not listed — leaded | Not listed — leaded |
The table explains the commercial tension in one line: CW602N solves corrosion but not lead, and CW617N solves neither for drinking water. If your programme must satisfy both, the answer is a lead-free DZR grade such as CW724R, not a switch between the two leaded brasses. Our lead-free brass specification guide covers the substitution route in detail.
The 2026–2028 rule changes buyers should plan for now
- EU Drinking Water Directive 2020/2184. Metallic materials in contact with drinking water are accepted by listed composition. The European positive lists apply from 31 December 2026; there is no leaded brass on them. National approvals already in place may continue to be used for a transition period, commonly cited as ending 31 December 2032 — confirm the position for your member state.
- Germany and the 4MS scheme. CW617N has been usable for drinking water under national approval; German manufacturer datasheets currently show conformity until 11 January 2028, with CW510L and CW724R listed as conforming after that date. Plan the changeover, do not discover it.
- UK. WRAS and Kiwa product approvals for DZR fittings remain the practical route; approval belongs to the finished product, not to the alloy.
- Australia and New Zealand. AS/NZS 4020 and AS 2345 apply, and the lead-free requirements under G12/AS1 Amendment 14 became the only acceptable solution from 2 May 2026.
- Singapore. PUB moves potable-water copper alloys to the 4MSI positive list from 1 March 2027; several currently accepted grades including CW602N are phased out for potable use.
The pattern is consistent: dezincification resistance is now the entry ticket, and lead-free composition is the differentiator. A supplier who can only offer CW602N is compliant today and exposed within two to six years.
How DZR is actually proven: ISO 6509-1
ISO 6509-1 is the accelerated test. A cross-sectioned specimen is polished, immersed in 1% copper(II) chloride solution at 75 °C for 24 hours, then re-sectioned perpendicular to the exposed face and measured under a microscope for the maximum depth of zinc loss.
The test produces a depth, not a verdict — the limit comes from the specification that calls it up. For CW602N, EN 12164 (rod) and EN 12165 (forging stock) set 100 µm in any direction. CW625N and CW626N are allowed 200 µm. AS 2345 in Australia and New Zealand applies the same corrosion mechanism with its own criteria.
Two practical points for buyers:
- Test the finished part where the standard says so. Heat treatment and the beta-phase distribution it creates are what make inhibited brass resistant, so a bar certificate alone does not prove a forged or machined body.
- Ask for the ISO 6509-1 report by batch, not a generic quality certificate, and check that it names the alloy, the test laboratory, the measured depth and the limit it was assessed against.
DZR is a material property. The WRAS, Kiwa, DVGW or ACS approval on a finished valve or fitting is a product approval, held by whoever places it on the market. Component suppliers provide the material evidence; the approval stays with the brand owner. Confusing the two is the most common mistake in European tender documents.
What to put in your purchase specification
A specification that says only “DZR brass” leaves the decision to your supplier. Write these nine lines instead:
- Alloy designation and temper, for example CW602N (CuZn36Pb2As), forged and heat treated.
- Dezincification resistance to ISO 6509-1, maximum depth 100 µm in any direction on the finished component.
- Material certificate to EN 10204 type 3.1 per heat, with chemical composition and mechanical properties.
- Maximum lead content, stated as a percentage, plus the market rule it satisfies (EU positive list, NSF/ANSI 372, AS/NZS 4020).
- Heat-treatment record: temperature, time and cooling method after forming.
- Marking requirement — CR, DZR or DR on the body where the size allows.
- Surface condition and any plating, since coatings must not obscure the section the test needs. See our guide to plating and corrosion protection for what plating can and cannot do here.
- Thread and dimensional requirements, with the gauge standard named — our tolerances and surface finish guide sets out the format.
- Inspection and sampling regime, including whether the DZR report is per heat, per batch or per shipment.
If you already run an incoming inspection plan, add the certificate check to it rather than creating a parallel system; the sampling logic in our AQL inspection guide applies unchanged to document review.
Where DZR pays for itself
Specify a DZR grade when any of the following is true:
- The part touches potable water and the market mandates DZR — the Netherlands, Scandinavia, the UK for concealed fittings, Australia and New Zealand.
- The supply is soft, low in carbonate hardness or high in chloride.
- Water sits stagnant or runs warm, such as dead legs, hot manifolds or seasonal buildings.
- The fitting is concealed, so a failure means opening a wall or a floor.
- The part is pressure-bearing and a leak carries a safety or warranty cost far above the material premium.
For a gas, pneumatic or neutral hard-water application, standard brass remains the sensible engineering and commercial choice. That trade-off is covered in our alloy selection guide.
Cost and machining: what changes on the shop floor
Three things move when you switch from CW617N to a DZR grade, and they all show up in the piece price:
- Material. Inhibited and especially silicon brasses carry a premium over free-cutting CW617N.
- Machinability. CW602N machines close to standard brass but not quite as freely; silicon brass CW724R is typically rated around 85% of CW617N, so cycle times lengthen and tool wear rises.
- An extra process step. Inhibited DZR needs the post-forming heat treatment, with furnace time, handling and a recorded cooling profile.
The offsetting savings are real too: lower warranty exposure, fewer field failures, and one specification that can serve several European markets instead of a different grade per country. Our breakdown of what drives brass CNC machining cost shows where the heat-treatment step sits in the total.
Seven questions to ask a DZR supplier
- Which alloy, and is it on the positive list for the market I am selling into?
- Do you supply an ISO 6509-1 report on the finished part, and what limit was it assessed against?
- Who performs the heat treatment, and can you show the record?
- What is the lead content, and what evidence supports the figure?
- Can you supply an EN 10204 3.1 certificate per heat?
- How do you segregate DZR and standard brass on the shop floor and in packing?
- Which product approvals do your customers hold with your components, and can you support a new approval submission?
Frequently asked questions
Is CW602N the same as DZR brass? It is the most widely specified DZR grade in Europe, but not the only one. CW625N, CW626N and the lead-free silicon brass CW724R are also DZR. Check the designation on the certificate, not the marketing word.
Can CW617N be used for drinking water? Under some national approvals for a limited period, yes; under the European positive lists applying from 31 December 2026, no — and it has no dezincification resistance regardless.
Is DZR brass lead-free? No. CW602N contains 1.7–2.8% lead. For lead-free plus DZR, specify CW724R or C69300.
How long does the ISO 6509-1 test take? The immersion is 24 hours; with sectioning, measurement and reporting, plan on one to two weeks at an accredited laboratory.
Does plating make standard brass acceptable for water? No. Plating is a barrier, not a metallurgical fix, and it is compromised at threads, cut edges and any damaged area.
Getting the grade right before the drawing is released
Most DZR problems are specification problems, not manufacturing problems: the drawing says “brass”, the purchase order says “CW617N”, and the market requires a lead-free DZR alloy that nobody wrote down. Fix that at the drawing stage and the rest follows.
Premi Brasscom International machines brass, copper, aluminium, stainless steel and gun metal components to drawing at our Dared, Jamnagar plant, with ISO 9001:2015 and IATF 16949 certification and EN 10204 3.1 material certificates per heat. If you are moving a potable-water part to a DZR or lead-free grade, send us the drawing and the market it is destined for and we will confirm the alloy route, the test evidence and the approval path before quoting.